
Technical comparison | Slurry isolation & RFQ
Resposta rápida: For slurry with settling or fibrous solids, a purpose-designed knife gate valve often deserves the first technical review; for comparatively clean process isolation, a wedge gate valve may be more appropriate. Neither choice follows from the valve name alone. Gate travel, particle interference, seat contact, packing condition, pressure direction and required differential pressure determine whether the offered valve can close, seal and remain serviceable. This comparison provides a preliminary selection framework and the supplier evidence needed before RFQ approval.
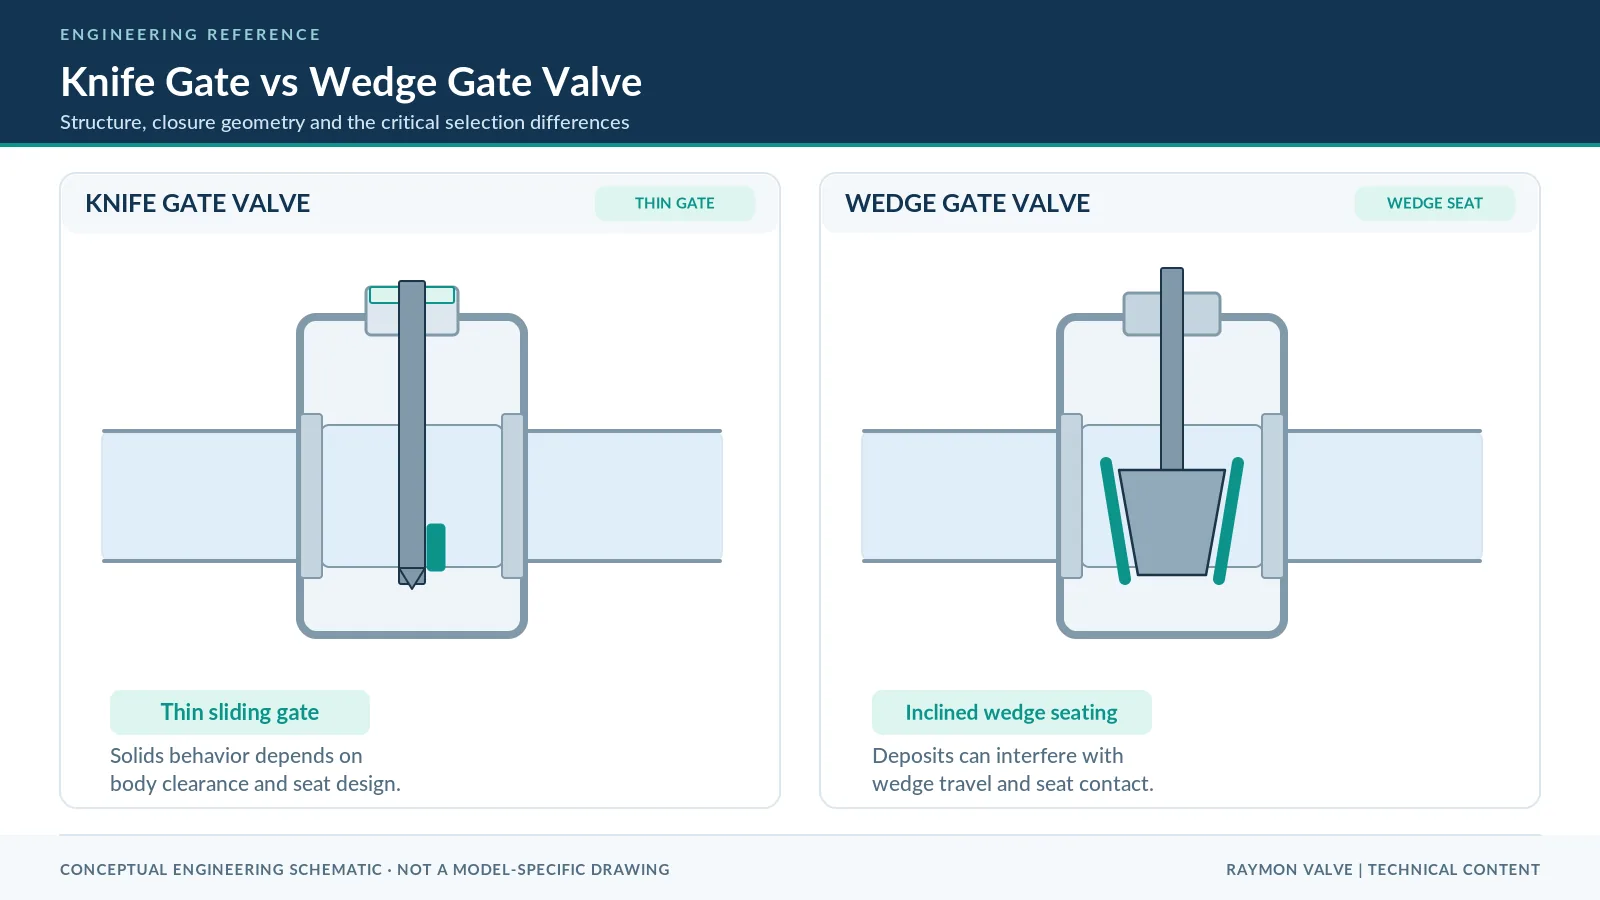
Knife Gate Valve vs Wedge Gate Valve: Quick Comparison
Both are linear-motion isolation valves, but their closure interfaces and typical risk profiles are different. Use this table for preliminary screening—not final approval.
| Decision point | Knife gate valve | Válvula gaveta cunha |
|---|---|---|
| Closure geometry | Relatively thin sliding gate | Wedge-shaped gate contacting inclined seats |
| Common evaluation | Slurry, solids-bearing and fibrous duties | Conventional process isolation |
| Comportamento de sólidos | Special designs can manage solids; still vulnerable to jamming and wear | Settled solids may obstruct wedge travel or seating |
| Seating | Resilient, metallic, sleeve-type or application-specific | Inclined seating interfaces; variant-dependent |
| External sealing | Moving-gate packing or stuffing box, construction-dependent | Stem packing and potentially a bonnet joint |
| Pressure direction | May be unidirectional or bidirectional | Verify the offered seat and sealing direction |
| Pressão diferencial | Must confirm pressure-boundary, shutoff and opening/closing limits separately | Same distinction; wedge loading and friction matter |
| Typical maintenance | Gate/seat wear, packing leakage, particle buildup | Wedge/seat damage, deposits, stem/packing wear |
| Evidência do fornecedor | Sectional drawing, solids review, seat/packing details, pressure-direction tests | Rating, wedge/seat drawing, operating-load and test data |
Preliminary rule: Start with a slurry-oriented knife gate design when solids management dominates the duty. Start with a suitable wedge gate design where clean or relatively clean process isolation dominates. At high differential pressure, with stringent leakage, or in severe abrasive service, neither family should be preapproved without evidence.
For broader construction options, see Raymon Valve’s industrial gate valves e Guia de Válvulas Gaveta.
How Do Knife and Wedge Gate Designs Handle Solids Differently?
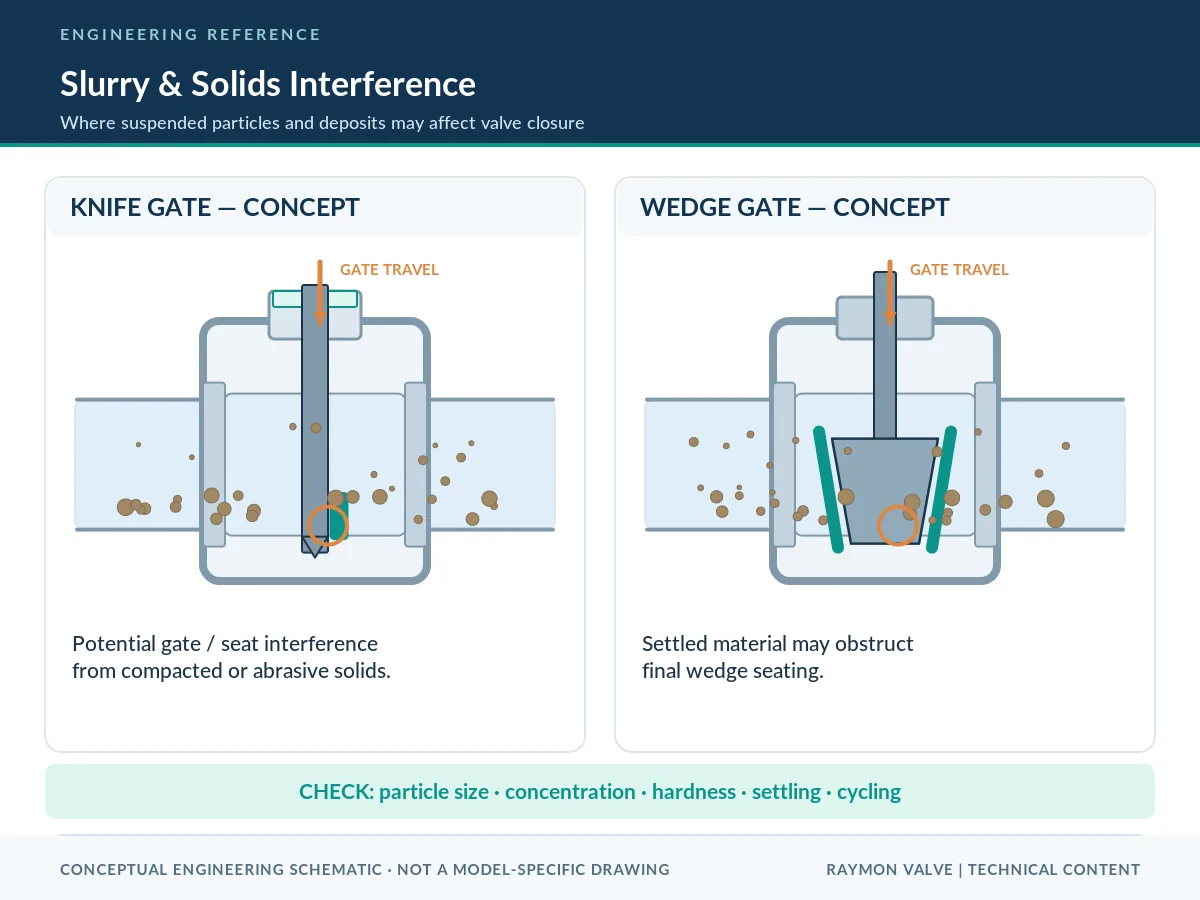
Thin Knife Gate and Solids Interference
A knife gate valve normally moves a relatively thin gate through the flow passage. Certain designs are arranged to displace a portion of the suspended solids as the gate moves into its seat region. This can be useful where conventional seating surfaces are exposed to deposits.
But a knife edge is not an unlimited cutting tool. Coarse particles, hard fragments, fibrous agglomerates and compacted deposits can increase closing thrust, damage sealing surfaces or stop the gate before full closure. Whether that happens depends on particle geometry, the lower body profile, contact clearances, pressure forces and seat construction.
Ask the supplier to provide the actual gate and seat sectional drawing, not just a catalog statement claiming the valve is suitable for slurry.
Wedge Geometry and Lower-Body Accumulation
A wedge gate moves toward inclined seating surfaces. Material retained in a lower body cavity or around the seating area may obstruct its final travel. Trapped particles can also interrupt uniform seat contact, cause scoring or produce unacceptable seat leakage.
That does not mean every wedge valve will fail with any suspended solids. Particle concentration, deposition rate, the body geometry, duty cycle and cleaning provisions can all change the result. A small quantity of non-settling fines is different from an abrasive slurry that consolidates during shutdown.
Gate Clearance, Flush Connections and Operating Duty
Two knife gate valves with the same DN/NPS may have very different clearances, sleeves, wear parts, gland arrangements and flushing provisions. Confirm whether the proposed flush or purge feature is actually included and specify its fluid, pressure, connection and operating sequence. Flushing cannot automatically compensate for unsuitable materials or inadequate clearance.
Which Valve Is Better for Slurry and Solids-Containing Service?
Solids Concentration, Size and Abrasiveness
The word slurry is too broad to complete a valve specification. Record concentration by mass or volume, particle-size distribution, maximum particle size, hardness, shape and settling tendency. Also identify the carrier liquid, pH, normal and upset temperatures, velocity and whether the material can crystallize, form scale or compact during shutdown.
A concentration value without particle characteristics is insufficient. Large angular particles may obstruct gate travel even at a modest average concentration, while hard fines at elevated velocity can erode a liner or seat. Ask whether the reported solids percentage represents a steady operating sample or a maximum including shutdown, restart and upset conditions.
Illustrative screening example — mineral slurry: A valve that travels freely during continuous flow may require greater closing load after sediment accumulates during a shutdown. The likely mechanism is deposit compaction in the gate/seat region, not an inherently defective actuator. Compare the expected idle duration, maximum particle size and gate clearance; then request manufacturer operating-load data for the restart/closure case before accepting either construction.
Settling Slurry, Fibrous Media and Deposits
- Settling mineral slurry: review the lower body, gate travel path, abrasive wear and ability to close after stagnation.
- Pulp and fibrous stock: review fiber accumulation, wiping contact, gate clearance and frequency of cycling.
- Wastewater sludge: review rags, grit, solids variation, flushing provisions and maintenance access.
- Scaling or crystallizing media: review solid deposits after temperature change or shutdown and whether repeated movement increases friction.
Each case may need a different knife gate configuration. A generic slurry label does not establish service approval.
For application and product scope, see the Knife Gate Valve product page. Confirm the offered construction against your slurry data and the project specification.
Velocity, Cycling and Stagnation Periods
Flow velocity can affect abrasive wear, but stagnant periods often govern the risk of settling and incomplete closure. Record whether the valve closes while the slurry is moving, after the line has stood idle, or during flushing or backwash. The relevant operating case may differ from the nominal process condition.
Frequent cycling adds repeated gate/seat contact and packing movement. A proposed purge or flush arrangement needs an available utility, a defined supply pressure and a documented operating sequence; a line item reading only “flushing available” is not sufficient for technical approval.
When Neither Standard Construction Should Be Approved
Severe abrasion together with high differential pressure, large obstructive particles, stringent shutoff, or frequent cycling may require a purpose-designed isolation valve, different wear components, specialized seating or another valve family. The correct decision is to request the manufacturer’s design rationale and defined service limits rather than select solely by valve type.
Illustrative Decision Path: Settling Slurry with Reverse-Pressure Cleaning
Illustrative scenario, not a project record: a slurry line operates normally in one direction, stands idle long enough for solids to settle, and periodically undergoes reverse-pressure cleaning. A preliminary preference for a knife gate valve is reasonable, but cannot be approved from the word “slurry” alone.
- Define the medium: supply solids loading, particle-size distribution, hardness and expected deposits after shutdown.
- Define each pressure case: normal isolation, reverse-pressure cleaning, closed-valve differential pressure and closing/opening under differential pressure.
- Check the actual construction: obtain a gate/seat section, packing and wiper arrangement, wear parts and any flush-port details.
- Set acceptance criteria: state seat leakage per pressure direction, shell and function tests, and service-specific limits requiring written confirmation.
- Compare bids: reject unaddressed deviations rather than treating the same nominal size and pressure designation as equivalence.
Limite de decisão: if the manufacturer cannot substantiate reverse-pressure shutoff or required operating force for the offered configuration, the design remains under review regardless of apparent slurry suitability.
Knife Gate vs Wedge Gate Valve Seat Design and Shutoff
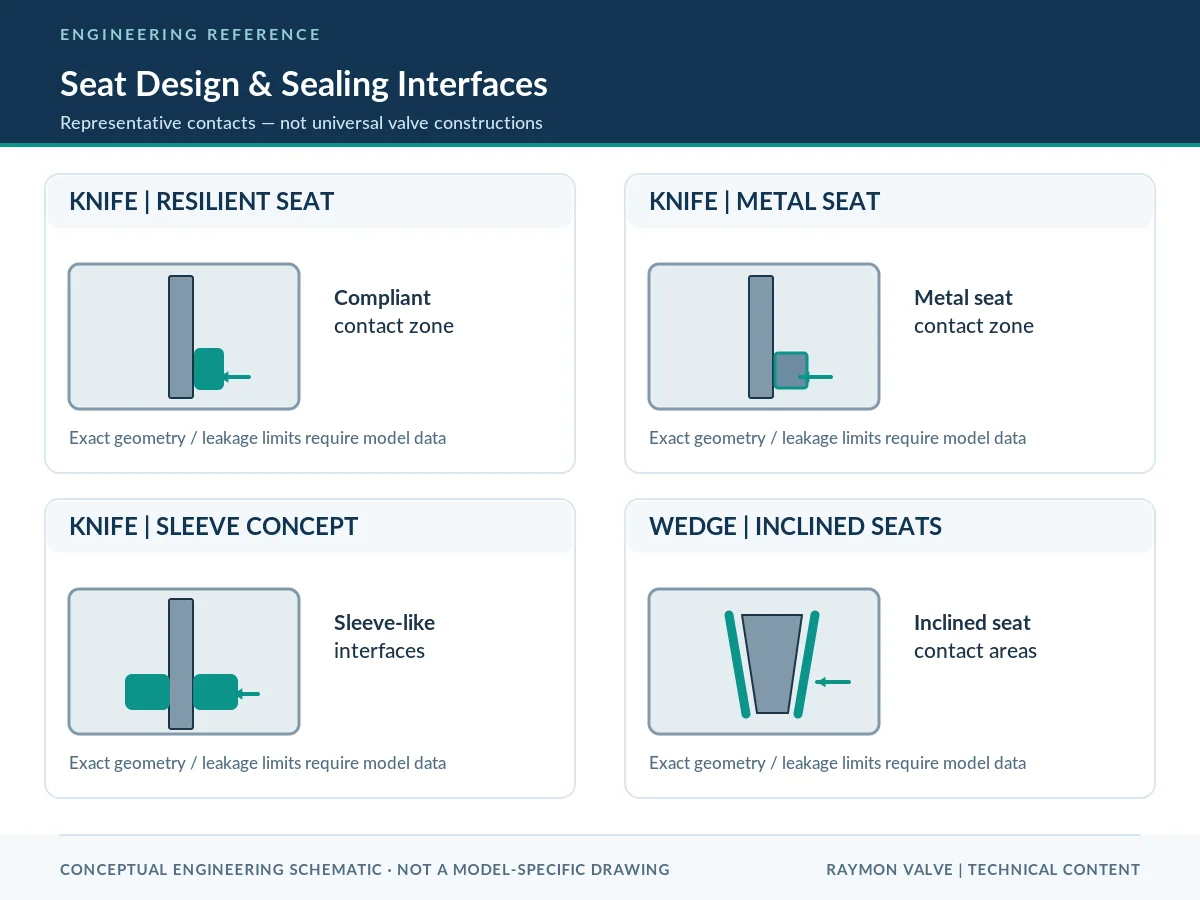
Resilient, Metallic and Sleeve-Type Knife Gate Seats
Resilient seats can provide compliant gate contact but must be reviewed for chemical compatibility, temperature, pressure, abrasion and deformation. Metallic seats may be selected for certain severe conditions, although leakage performance and the risk of scoring depend on the exact interface and acceptance criteria. Sleeve-type designs can use replaceable sealing or wear elements; their geometry and pressure behavior vary widely between models.
There is no universally superior seat material. A supplier should identify the contact geometry, material grade, replaceable components, service limits and approved pressure direction.
Wedge Seating Contact and Deposits
Wedge gate closure depends on the gate engaging inclined seats. Geometry, friction, stem thrust, temperature, differential pressure and surface condition can influence the resulting load. Solid, flexible and split-wedge configurations should not be assumed equivalent. Abrasive particles trapped during the final closing stroke can produce seat damage even where the nominal pressure class appears adequate.
Illustrative failure review — incomplete wedge seating: A closed-position signal does not prove that the wedge established the specified seat contact when grit remains in the lower body. Confirm actual travel, permitted inspection observations and the defined seat-leakage test after safe isolation. If solids repeatedly interfere, review body geometry or an alternative isolation construction rather than simply increasing actuator force.
Define Seat Leakage in the RFQ
Terms such as “tight shutoff” and “bubble-tight” are incomplete without a defined test. Specify test standard and contractual edition, test medium, pressure and duration, applied pressure direction, allowable seat leakage, and witness/hold points. A clean-fluid factory seat test demonstrates a stated new-valve acceptance condition; it does not establish future abrasion life or unchanged shutoff after solids have crossed the sealing interface. For bidirectional duty, request acceptance evidence for each required pressure direction.
Packing Design, Stem Sealing and External Leakage Risks
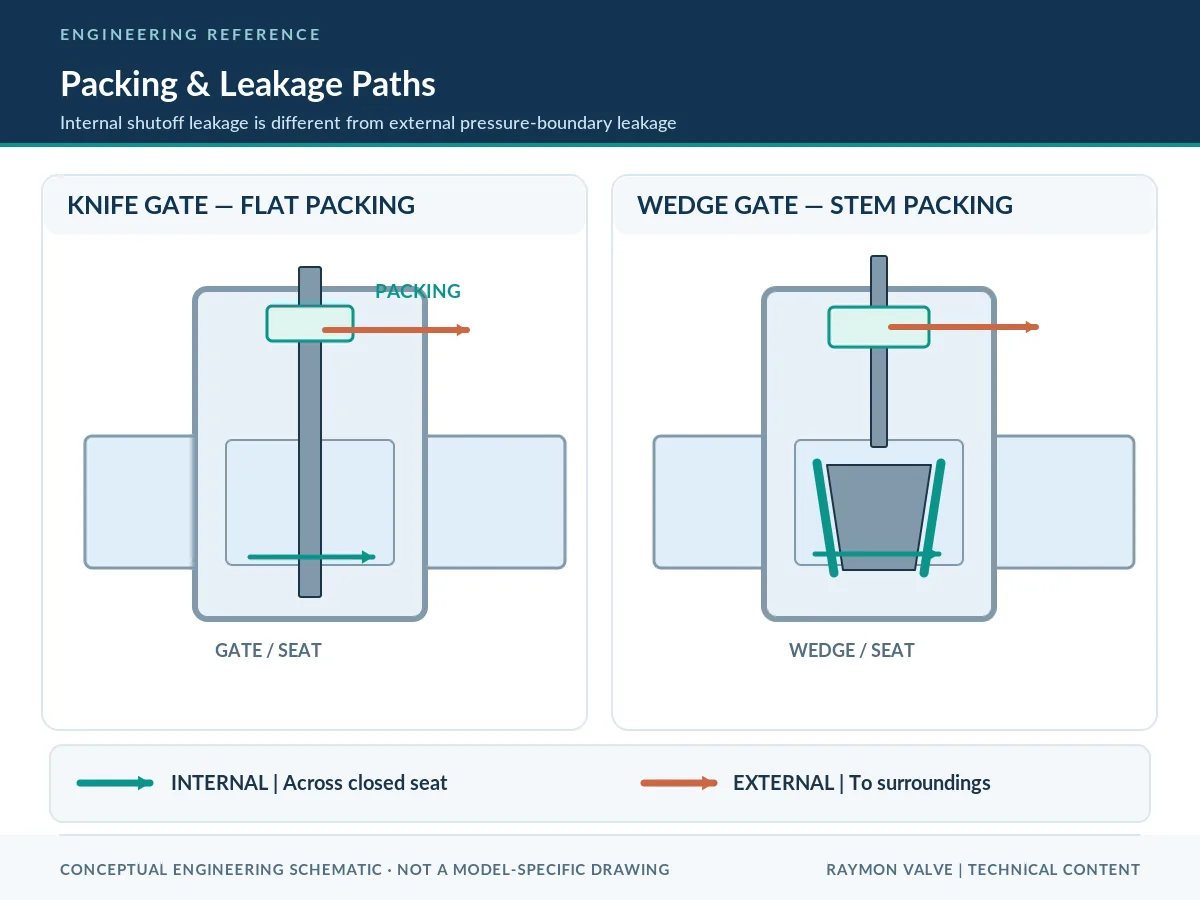
Knife Gate Packing and Sliding-Gate Wear
Many knife gate constructions seal around the moving gate using a stuffing box and gland. Solids carried on the gate surface may enter or abrade the packing region, depending on wipers, surface finish, gland compression and the available flush provisions. This may increase operating friction or contribute to external leakage.
Illustrative inspection example — packing scope: Two quotations may both specify “replaceable packing,” yet one may omit accessible gland clearance, wiper details or the packing grade. Those omissions matter when abrasive slurry is expected to coat the moving gate. Review the assembly drawing and bill of materials, confirm the replacement procedure and permitted gland loading, and record any difference as a technical clarification rather than assuming equivalent external-leakage performance.
Wedge Gate Stem Packing and Bonnet Joints
Conventional bonneted wedge gate valves generally use stem packing. The body-to-bonnet interface is a separate external pressure-boundary seal. Stem alignment, finish, packing material and operation frequency all matter; the exact leakage paths differ from those of bonnetless knife gate configurations.
Internal Seat Leakage Is Not External Packing Leakage
| Leakage path | What it means | Required review |
|---|---|---|
| Across closed seat | Internal leakage through the isolated passage | Seat design and closure test criteria |
| Along moving gate or stem packing | Process fluid escapes externally | Packing design, condition and maintenance method |
| Bonnet or pressure joint, where present | External pressure-boundary leakage | Gasket/joint design and inspection |
A valve may pass its seat test yet be unsuitable for an external leakage requirement. Conversely, externally tight packing does not establish acceptable isolation across the gate.
Maintenance boundary: Packing adjustments or disassembly should only follow the manufacturer’s procedure and the plant’s isolation, depressurization and draining rules. Excessive gland compression can increase operating force; it is not a universal leakage remedy.
Pressure Direction and Bidirectional Sealing: What Must Be Verified?
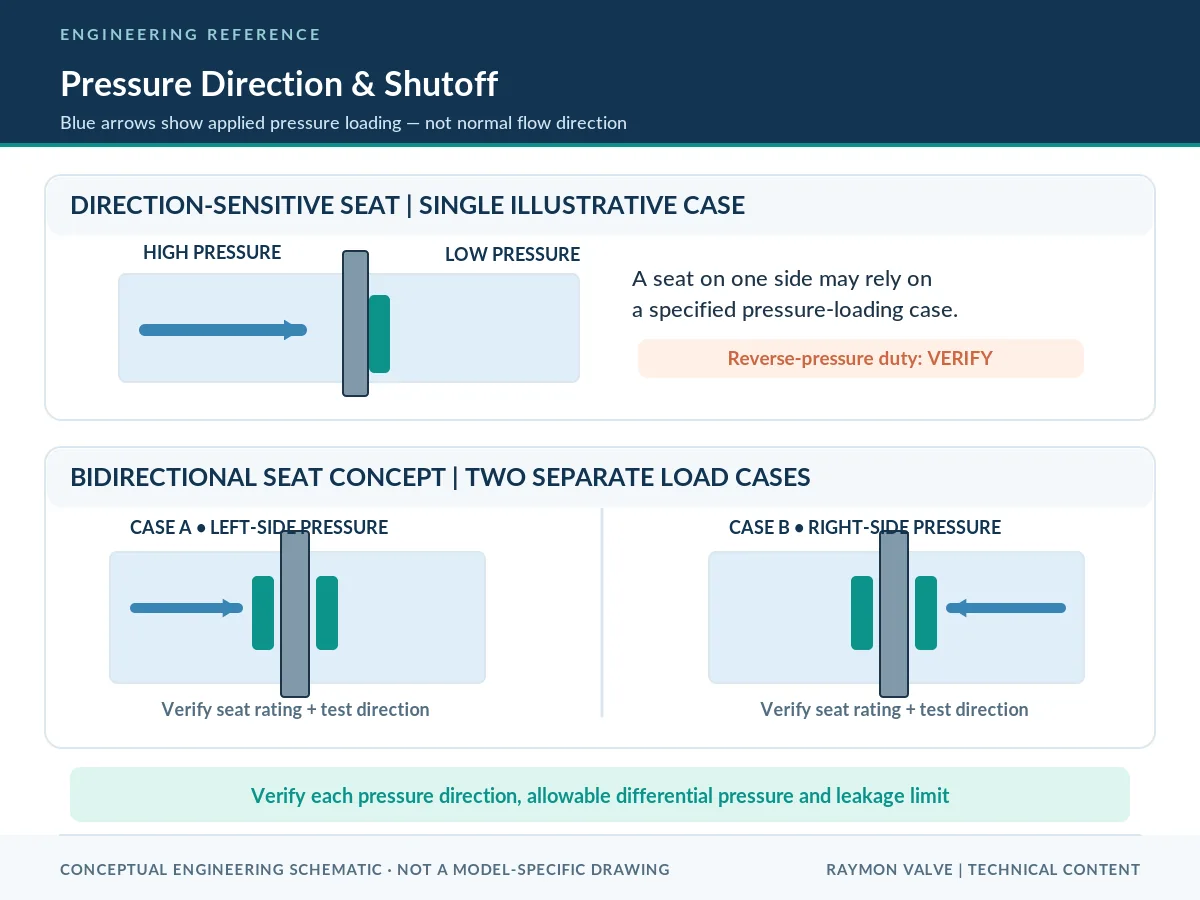
Flow Direction Is Not the Same as Pressure-Sealing Direction
A line has a normal flow direction, but a closed valve may see reverse differential pressure during pump shutdown, backwash, line draining or maintenance. The critical question is which side applies pressure while the valve is closed and under what leakage acceptance requirement. A generic arrow does not establish the full sealing envelope.
Pressure-case check: A valve may close against forward flow during normal shutdown but face pressure from the opposite side during line backwash. Specify the pressurized side, maximum differential pressure, duration and leakage criterion for both closed-valve states. Separately state whether opening or closing under that differential pressure is required; a bidirectional seat designation alone cannot validate the operator or actuator load case.
Unidirectional and Bidirectional Knife Gate Designs
Some knife gate seats are intended for a specific pressure side, while others provide bidirectional shutoff within documented limits. For a direction-sensitive construction, seat orientation and installation instructions are essential. For a bidirectional version, verify both pressure directions, allowable differential pressure and the corresponding test evidence. The two directions should not be assumed to have identical ratings.
Evidence example (third party only): A published bidirectional knife gate valve product description documents one manufacturer-specific construction using a replaceable elastomer seat. This demonstrates that seat configuration and sealing direction are design-dependent; it is not evidence of Raymon Valve product ratings, approval or test results. Obtain the exact offered model’s seat drawing and pressure-direction test requirements.
Closed-Valve Differential Pressure vs Closing Differential Pressure
Three distinct ratings or duties must be documented: (1) the maximum differential pressure retained after the valve has closed, (2) the differential pressure against which the gate must move during closing, and (3) the differential pressure against which it must open. These cases may place different loads on the gate, seat and packing. Request the exact-model thrust or torque basis for each required operating condition and identify the direction of pressure application.
Dead-End Duty and End Connections
End-of-line or dead-end service can impose different pressure and support conditions if downstream piping is absent. Wafer, lugged and flanged terms alone do not prove dead-end capability. Request the approved installation drawing, bolting/connection arrangements and pressure and test basis for that duty.
| Pressure case to specify | Buyer must define | Supplier must demonstrate |
|---|---|---|
| Normal isolated condition | Pressurized side, maximum closed differential pressure and leakage target | Seat side, shutoff rating and test basis for that direction |
| Reverse or backwash condition | Reverse pressurized side, expected duration and leakage target | Reverse-pressure seat rating and acceptance evidence; no automatic equivalence |
| Closing or opening under load | Maximum required differential pressure and operating time | Exact valve opening/closing thrust or torque data and limitations |
| Pressure-temperature design case | Design pressure, temperature and material/piping specification | Applicable pressure-boundary rating and documented configuration |
| Downstream pipe removed / dead-end duty | Which flange is unsupported, retained pressure and maintenance arrangement | Approved end-of-line connection, bolting, support and pressure limits |
Pressure Rating, Temperature, End Connections and Actuation
Do Not Confuse Pressure Class with Shutoff Capability
A pressure-temperature rating addresses the pressure boundary under the applicable material and design rules. A shutoff differential-pressure limit describes the supported sealing condition; an operating differential-pressure limit describes the available load for opening or closing. All three must be verified for the offered configuration.
Not every knife gate valve is a low-pressure product. Dedicated high-pressure knife gate design requirements exist, including MSS SP-135. Their existence does not establish a higher rating for any unspecified model.
End Connections, Orientation and Piping Integration
Check DN/NPS, Class/PN, flange or end-connection standard, face-to-face dimension, gasket system, bolting and available space. In slurry duty, also evaluate the installed orientation, drainage, maintenance access and support loads. Do not infer the approved pressure or sealing configuration solely from an end-connection name.
Operating Thrust and Actuation
Valve size alone cannot establish actuator capacity. Ask for the manufacturer’s opening, running and closing force or torque under each governing pressure-direction case, including seat friction, packing friction, temperature and any credible solids-related resistance. Specify operating time, cycle frequency, supply pressure or electrical power, ambient conditions, required failure response and manual override. The supplier must document the actuator matching basis and margin; no final actuator size is calculated in this article.
Common Failure Modes and Maintenance Considerations
| Symptom | Mecanismo possível | Verification before repair |
|---|---|---|
| Failure to fully close | Solids accumulation or mechanical obstruction | Travel indication, operating-load trend, safe internal inspection |
| Increasing seat leakage | Trapped particles, abrasion, damaged seal | Approved leakage test and seat examination |
| External packing leak | Wear, contamination, misalignment or incorrect compression | Packing/gland inspection after safe isolation |
| High operating load | Differential pressure, friction, buildup or component damage | Actual operating case and manufacturer load data |
| Recurring jamming | Particle size, sedimentation, inadequate clearance | Solids data and sectional geometry review |
| Excessive maintenance frequency | Cycling, abrasion, unsuitable materials or flushing | Wear history and design review |
This is a cause-and-verification matrix, not authorization to loosen or remove pressure-containing components while in service. Follow site isolation procedures and the manufacturer’s instructions.
Applicable Standards, Tests and Supplier Evidence
Standard names should be tied to the exact offered construction. Product-design requirements, shell tests, seat closure tests, functional tests and optional inspection activities are not interchangeable.
| Official reference | What it covers | What it does not establish |
|---|---|---|
| MSS SP-81-2021 | Specified stainless-steel or stainless-lined, bonnetless, flanged knife gate valves (including 2022 errata) | Conformity or suitability of every knife gate design |
| MSS SP-148-2023 | Specified low-pressure, bonnetless, unlined knife gate valves of carbon steel, iron or ductile iron construction | Application to lined/sleeved variants or high-pressure duty |
| MSS SP-135-2021 | Specified high-pressure knife gate valve constructions (including errata) | A high-pressure rating for an unspecified model |
| MSS SP-146-2024 | Specified iron high-pressure wafer- and flange-type knife gate valve constructions within its stated flange-compatibility scope | A universal high-pressure rating or applicability to all materials and end connections |
| MSS SP-151-2021 | Knife gate valve shell and seat closure pressure-test requirements | Long-term abrasion life or guaranteed in-service tightness |
| API 600 (14th edition listed by API) | Specified steel, bolted-bonnet gate valves with flanged or butt-welding ends; the currently listed edition must still be checked against the purchase specification | Coverage of every wedge gate valve construction or approval to an unpublished revision |
| ASME B16.34 | Applicable valve pressure-temperature and construction requirements; ASME lists the 2025 edition | Slurry compatibility or a particular seat’s performance |
| AWWA C520-24 | Knife gate valves within the specified waterworks application scope | Suitability for all industrial slurry services |
Edition and acceptance note: The purchaser’s contractual edition, valve standard scope, testing method, leakage acceptance and applicable supplements govern the technical bid. Standards references are not statements of product-specific certification.
For standard editions and applicability, consult the official publisher links in the matrix above. Additional testing context is available in Raymon Valve’s Valve Pressure Testing resource; the project test plan and applicable standard remain authoritative.
Pressure Tests and Documentation Must Be Separate Line Items
Specify shell pressure testing, closure/seat testing, functional testing, NDT, PMI, material certificates and third-party witnessing as separate deliverables where applicable. A shell test primarily checks the specified pressure-containing boundary; a seat test assesses shutoff under stated test conditions, not in-service wear. PMI supports positive alloy identification but does not replace a complete material test certificate, heat-treatment record or tag-to-part traceability. State the ITP witness and hold points, approved test direction and acceptance method, report format and deviations before order release.
What Evidence Is Needed at Each Approval Gate?
| Approval gate | Buyer / EPC requirement | Supplier deliverable |
|---|---|---|
| Before technical quotation | Complete service envelope, solids and chemistry, design conditions, pressure directions, cycle duty and applicable specifications | List of missing data or qualified assumptions; proposed product family and explicit exclusions |
| Technical bid acceptance | Defined pressure/seat leakage cases, materials, connection and actuation duty | Exact-model GA and sectional drawings, seat and packing details, rated limitations, load basis and signed/recorded deviations as specified |
| Inspection / release for shipment | Approved ITP, hold or witness points, test criteria and documentation list | Applicable shell, seat and functional test reports, material records and inspection documents as contractually required |
Evidência de limite: a catalog, generic type test or conformity statement should not be substituted for the exact-model documents and purchase-order acceptance required by the project. A factory pressure test does not demonstrate in-service abrasion life. The representative sectional graphics in this article are explanatory concepts; no Raymon Valve model-specific cutaway, seat-pressure test record or field-performance report has been provided for verification.
Knife Gate vs Wedge Gate Valve Selection Matrix and RFQ Checklist
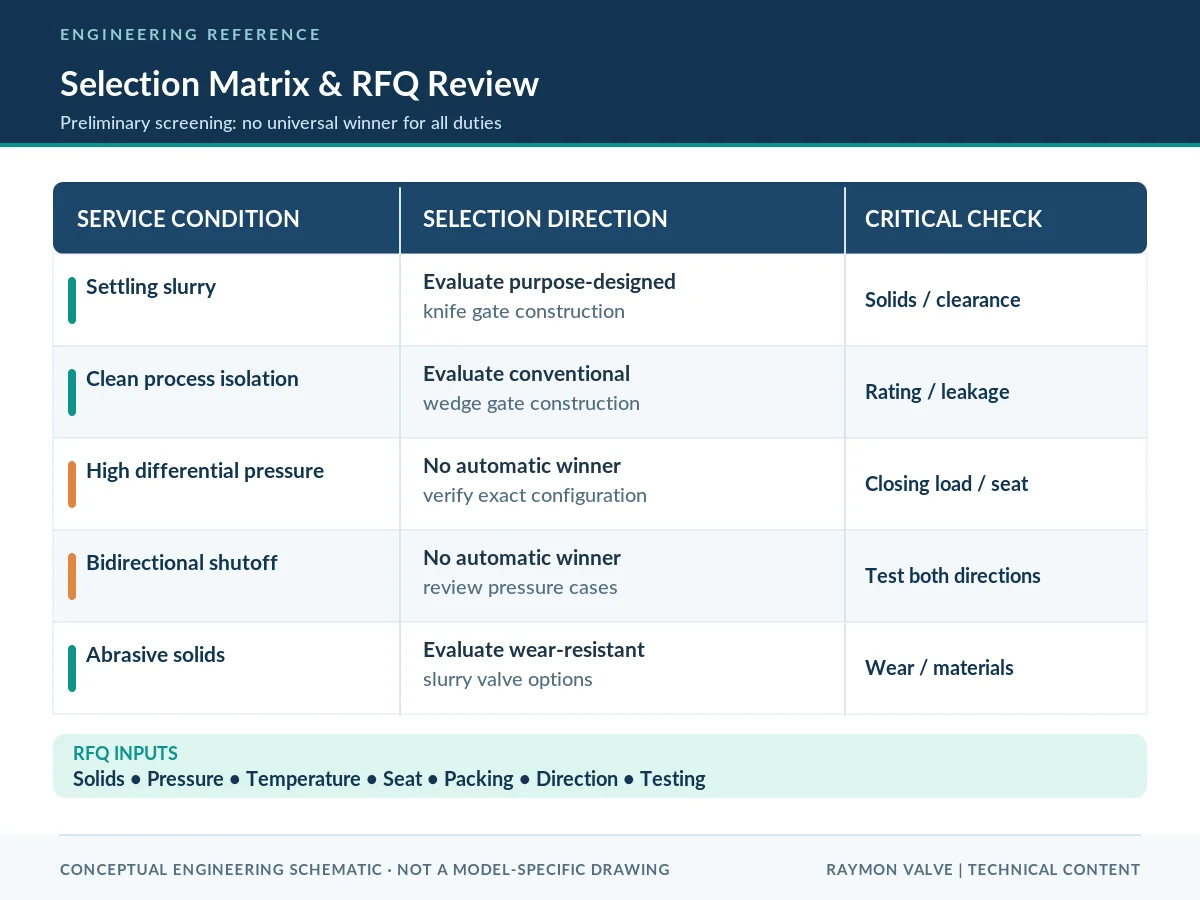
Matriz de Seleção Preliminar
| Condição de serviço | Direção preliminar | Verification that changes the decision |
|---|---|---|
| Settling slurry with significant solids | Evaluate a purpose-designed knife gate | Particle characteristics, gate/seat clearance, flushing |
| Fibrous or pulp-bearing medium | Evaluate a service-specific knife gate | Wiping contact, gate travel, seat geometry |
| Relatively clean process isolation | Evaluate a wedge gate | Piping class, pressure-temperature, seating |
| Severe abrasive slurry | Specialized slurry-isolation review | Wear parts, liners, material suitability |
| High shutoff differential pressure | No automatic winner | Exact pressure and sealing limits |
| Bidirectional isolation | Design-specific | Two directions, acceptance and testing |
| High cycling in contaminated media | Detailed design review | Operating load, packing, wear basis |
| End-of-line duty | Approval of exact configuration | Dead-end rating, installation, testing |
Minimum RFQ Data
| Buyer input | What the supplier must clarify |
|---|---|
| Medium, chemistry and temperature | Material and seal compatibility |
| Solids loading (% by mass or volume), particle sizes, hardness, settling and stagnation time | Gate/seat geometry, abrasion, obstruction, shutdown restart considerations |
| Flow velocity and normal/upset operating conditions | Wear mechanism and requested construction, liner or replaceable wear-part justification |
| Design pressure and normal pressure | Base da classificação de pressão-temperatura |
| Maximum opening/closing differential pressure | Operating thrust and limitations |
| Normal, reverse and dead-end pressure cases; allowable seat leakage | Seat-side drawing, limits and test evidence separately for each required direction |
| DN/NPS, Class/PN and end connection | Dimensional and pressure-boundary compatibility |
| Gate, seat, packing and liner requirements | Materials, service limits and replaceable parts |
| Manual, electric, pneumatic or hydraulic duty | Operating-load and actuator matching evidence |
| Cycling and cleaning/flush requirements | Maintenance design and utilities |
| Tests, ITP, MTC, NDT/PMI, witness points | Documentary deliverables and deviations |
Normalize Technical Quotations Before Price Comparison
A lower price is not a technically equivalent offer when reverse-pressure shutoff, operating load or test acceptance remains undefined. Commercial comparison should follow the technical disposition of deviations, not precede it.
Bid-normalization example: One offer may provide a direction-sensitive seat and another a bidirectional seat, while both list the same nominal size and pressure designation. Compare each against the actual reverse-pressure acceptance requirement and submitted seat schematic. If the first bid does not demonstrate required reverse-direction shutoff, classify it as Clarification Needed or a documented Qualified Deviation—not as fully compliant based on matching catalog labels.
Assign a technical bid disposition for each material requirement:
- Comply: The exact offered design and submitted evidence meet the stated acceptance criterion.
- Clarification Needed: A requirement may be met, but a drawing, rating, test direction or document is missing; approval remains pending.
- Qualified Deviation: The supplier explicitly identifies a difference with its proposed alternative; the purchaser must evaluate and approve or reject it in writing.
- Reject: The proposal demonstrably fails a mandatory safety, pressure-boundary, isolation or other non-negotiable project requirement.
Record the status and evidence reference in the technical bid tabulation before evaluating commercial offers.
Final Selection: When to Choose Each Design
Escolha uma purpose-designed knife gate valve for further review where solids, deposits or fibers make conventional wedge seating problematic—subject to pressure-direction, abrasion, packing and shutoff confirmation. Evaluate a wedge gate valve where the principal duty is conventional process isolation, the medium is compatible and the proposed construction meets the piping specification and operating envelope.
If high differential pressure, end-of-line isolation, severe abrasive wear, strict leakage or unusual cycling dominates the application, request project-specific evaluation rather than declare either valve family the winner.
For a separate comparison centered on pipeline bore geometry and pigging, see Wedge Gate Valve vs Slab Gate Valve.
Procurement rule: Approve the actual valve design from the completed datasheet, gate/seat drawing, service conditions, pressure-direction evidence, operating-load information, test scope and declared deviations—not from the family name alone.
PROJECT-SPECIFIC REVIEW
Request Knife Gate Valve Selection Review
Send the service medium and solids data, design pressure and temperature, normal and reverse pressure-direction cases, maximum closed and operating differential pressures, required seat leakage, preferred seat and packing materials, piping connection, cycling duty and test/documentation requirements. Ask for a comparison of the proposed valve construction, evidence still needed and any supplier deviations before technical approval.
Submit Your Valve Datasheet & RFQPerguntas Frequentes
What is the main difference between a knife gate valve and a wedge gate valve?
A knife gate generally uses a relatively thin sliding gate, whereas a wedge gate uses a wedge-shaped closure against inclined seat surfaces. That affects solids interference, seat geometry and operating load. Performance depends on the actual valve construction and service conditions.
Is a knife gate valve better for slurry and solids?
A purpose-designed knife gate may be the better initial candidate for many settling, fibrous or solids-bearing duties, but the decision must account for particle characteristics, abrasion, differential pressure, required leakage and packing design.
Can a wedge gate valve handle slurry?
Some wedge constructions may handle limited contamination, but settling or abrasive solids can obstruct travel or damage seats. Review solids loading, body geometry, operating frequency and allowable leakage before accepting the design.
Are knife gate valves bidirectional?
Some knife gate valves are direction-sensitive, while others are designed for bidirectional shutoff. The exact model must document its seat arrangement, leakage criteria and maximum differential pressure for each required direction. Bidirectional sealing does not automatically establish equal ratings or acceptable opening/closing loads in both directions.
Why do knife gate valves experience packing leakage?
Potential causes include gate-surface wear, abrasive contamination, packing degradation, misalignment, frequent movement or incorrect gland loading. Diagnosis and adjustment require safe isolation and the manufacturer’s maintenance procedure.
What information is required to select a knife gate valve for abrasive slurry?
Provide slurry chemistry, solids concentration (mass or volume basis), particle-size distribution, hardness and settling tendency; normal, design and upset pressure-temperature cases; maximum closed-valve and operating differential pressure; required sealing directions; DN/NPS, connection, leakage criteria, cycling and actuator duty. Request the offered gate/seat and packing drawings, applicable test criteria and a technical deviation schedule.
Nota de Engenharia
This guide supports preliminary engineering screening and B2B technical bid comparison. It does not certify a specific Raymon Valve model, replace a manufacturer-approved datasheet, establish an actuator size, or prove suitability for any particular slurry. Final selection and acceptance must follow verified process data, applicable codes, the purchase specification and the offered design and test documentation. Example scenarios and engineering diagrams are illustrative, not records of Raymon Valve customers, validated test outcomes or approved manufacturer drawings.
For company background and general contact information, see Sobre a Raymon Valve.
 Portuguese
 English
 German
 Arabic
 French
 Spanish
 Italian
 Russian